October 13, 2026
When we help customers solve excessive pressure drop, unstable flow, or premature filter blockage, we begin with the pore structure—not only the nominal micron rating. In this guide, I will show you how to evaluate pore size distribution, porosity, permeability, layer thickness, and filtration velocity, then convert the results into a practical specification for a JINTAI Sintered Porous Asymmetric Filter Element. By following the steps below, you can reduce trial-and-error, improve equipment efficiency, and select a filter that delivers predictable pressure performance.
Pressure drop, or ΔP, is the pressure difference between the upstream and downstream sides of a filter. It represents the energy required to push a gas or liquid through the porous metal structure.
For a clean porous filter, pressure drop is mainly influenced by:
A simplified Darcy equation is commonly used at low flow velocity:
[ \Delta P = \frac{\mu L v}{K} ]
Where:
At higher velocities, inertial resistance also becomes important. Engineers may then use the Darcy–Forchheimer relationship:
[ \Delta P = \frac{\mu L v}{K} + \rho \beta L v^2 ]
Here, ρ is fluid density and β is the inertial coefficient.
This explains why a small increase in flow velocity can create a disproportionate increase in pressure drop. It also explains why two metal filters with the same nominal rating can perform very differently.
A conventional sintered filter may have a relatively uniform pore structure throughout its wall. An asymmetric filter uses a graded structure, with different pore sizes or densities across the filtration direction.
A typical cross-section may look like this:
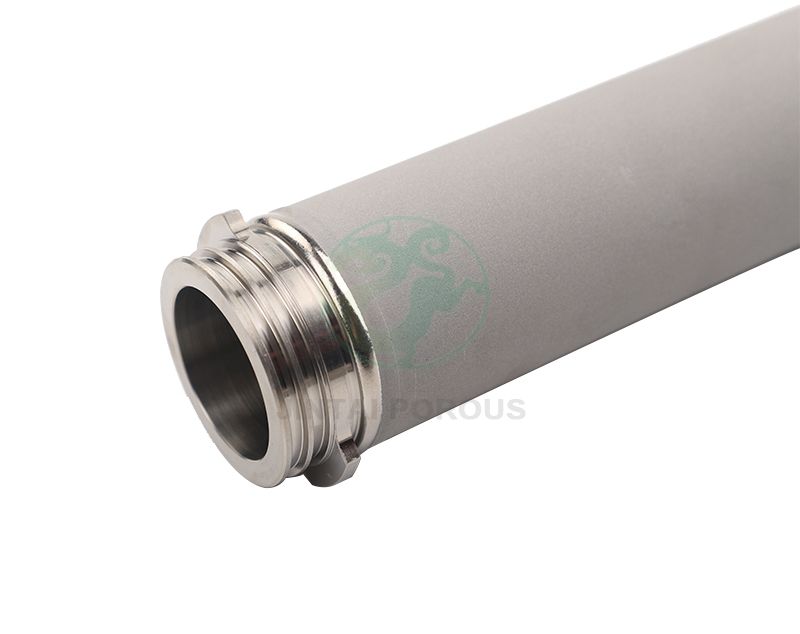
The fine layer controls particle retention, while the coarse support layer reduces hydraulic resistance. This design allows a Sintered Porous Asymmetric Filter Element to provide high filtration efficiency without making the entire filter wall unnecessarily dense.
The key is balance. If the fine layer is too thick, pressure drop rises. If the support layer is too open or poorly bonded, the element may lose mechanical strength or develop nonuniform flow.
The surface filtration layer generally has the smallest effective pores. These pores determine:
The internal support layer normally contains larger interconnected pores. Its role is to maintain:
This graded pore architecture is the central reason How Pore Structure Affects Pressure Drop in Asymmetric Metal Filters must be considered during design rather than after production.
As pore diameter decreases, the available flow channels become narrower. For many porous structures, permeability decreases rapidly as pore size decreases.
A filter with a 1-micron surface layer will generally create more resistance than a filter with a 10-micron surface layer, assuming the same thickness and porosity. However, the actual pressure drop depends on the entire pore-size distribution, not just the largest or smallest pore.
A specification should therefore include:
Porosity is the percentage of open volume within the porous metal. Higher porosity generally means more flow channels and lower resistance.
However, excessive porosity can reduce:
For this reason, we do not recommend choosing the highest possible porosity without checking operating pressure and structural requirements.
Tortuosity describes how winding the internal flow path is. A straight, interconnected pore network offers less resistance than a narrow, highly irregular network.
Two elements can have the same porosity and nominal pore size but different pressure drops because their pore geometry and tortuosity are different. This is one reason permeability testing is more useful than relying on pore-size data alone.
The fine filtration layer is essential for retention, but its thickness must be controlled. A thick fine layer increases the length of the restrictive flow path.
An asymmetric construction solves this problem by placing filtration precision where it is needed while using a more permeable support structure behind it. In practical applications, this can reduce clean pressure drop compared with a uniformly fine sintered element.
A narrow pore distribution can provide consistent filtration but may load quickly when the process contains a wide range of particle sizes. A graded structure can capture particles progressively and reduce rapid blinding.
Surface cake formation can either help or hurt performance:
This is why How Pore Structure Affects Pressure Drop in Asymmetric Metal Filters must be evaluated under both clean and contaminated conditions.
Before requesting a quotation or technical drawing, collect the following information:
For example, a liquid process with 20 cP viscosity will normally produce a higher pressure drop than water at the same velocity. Gas filtration may require correction for compressibility and pressure conditions.
Do not select a filter only by micron rating. Establish a clean ΔP limit and a maximum operating ΔP limit.
A practical specification may state:
The actual values must be calculated from the process. The important point is to define them before selecting the pore structure.
Work with the manufacturer to determine:
For a high-flow process, increasing the effective filter area is often more reliable than simply selecting a more open pore structure. Increasing area reduces superficial velocity and therefore lowers pressure drop.
The relationship is straightforward:
[ v = \frac{Q}{A} ]
Where Q is volumetric flow rate and A is effective filtration area.
If the pressure drop is too high, we can often solve the problem by increasing surface area, reducing velocity, or modifying the support layer rather than sacrificing particle retention.
A supplier should provide test data that connects pore structure with hydraulic performance. Depending on the application, request:
ASTM E128 can be used for maximum pore diameter and permeability evaluation of rigid porous filters. ASTM B328 is relevant for density and porosity testing of sintered metal products. Bubble-point testing may be specified using an applicable ASTM or ISO procedure based on the liquid, gas, and filter geometry.
The test fluid, temperature, pressure, and reporting units must be documented. Permeability values are not directly comparable when one supplier tests with air and another tests with water.
Pressure drop is only one part of filter performance. The selected JINTAI Sintered Porous Asymmetric Filter Element must also withstand the process environment.
Review:
For high-temperature or corrosive service, material compatibility should be confirmed using the actual chemical concentration and operating temperature—not only the chemical name.
Laboratory permeability is useful, but production performance should be confirmed under realistic conditions.
A practical validation plan includes:
Where dimensions are critical, specify inspection precision to 0.01 mm for relevant diameter, length, flatness, or connection features. A supplier quality plan may also include 100% visual and dimensional inspection, batch traceability, and a documented certificate of conformity.
| Design feature | Uniform sintered structure | Asymmetric sintered structure |
|---|---|---|
| Filtration layer | Same or similar pore size throughout | Fine surface layer with coarse support |
| Clean pressure drop | Can be high when fine rating is required | Often lower when properly optimized |
| Particle retention | Consistent | Controlled by the fine layer |
| Support efficiency | May use restrictive material through full thickness | Permeable support layer improves flow |
| Fouling behavior | Can blind through the wall | More suitable for surface-loading designs |
| Manufacturing control | Relatively straightforward | Requires tighter layer and bonding control |
| Design flexibility | Moderate | High |
The asymmetric design is not automatically better in every application. Poorly controlled transitions, excessive fine-layer thickness, or uneven sintering can produce localized resistance. This is why supplier process control is essential.
Likely causes include:
Recommended actions:
Likely causes include:
Recommended actions:
Possible causes include:
For a JINTAI production program, request batch-level permeability records and serial-number traceability. For critical equipment, a 100% leak or integrity inspection is more appropriate than relying only on a sampling plan.
A reliable filter-development program uses both design calculations and measurement tools.
Useful resources include:
For dimensional control, record measurements to 0.01 mm where appropriate. For process monitoring, establish a response procedure—for example, reviewing abnormal pressure-drop data within 24 hours and identifying whether the cause is process contamination, installation error, or filter variation.
When we prepare a specification for a JINTAI Sintered Porous Asymmetric Filter Element, we recommend including the following information in the purchase document:
This level of detail prevents a common purchasing problem: receiving a filter that meets the nominal micron rating but fails the actual pressure-drop requirement.
Before approving your next asymmetric metal filter, we recommend that you:
Understanding How Pore Structure Affects Pressure Drop in Asymmetric Metal Filters enables us to select the right balance between retention, permeability, strength, and service life. With a controlled JINTAI Sintered Porous Asymmetric Filter Element, documented test conditions, and real-world validation, businesses can reduce pump and compressor energy losses, prevent unplanned shutdowns, and maintain stable product quality. Begin with your operating data, define the pressure-drop target, and ask JINTAI to engineer the pore structure around the complete process—not just the advertised micron rating.